As an oil seal supplier who’s spent 12 years on the factory floor, fielding panic calls from maintenance managers at 2 a.m. and walking line teams through reworks when shipments miss specs, I’ve learned oil seal problems aren’t just random failures—they’re a mix of design missteps, installation shortcuts, and plain old neglect that snags even the most experienced teams. Today, I’m breaking down the most common issues we spot, how they show up in the real world, and what every user should watch for to avoid costly downtime. Oil Seal
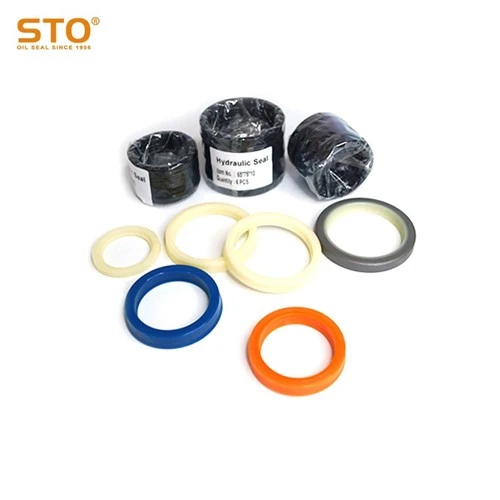
1. Lip Wear: The #1 Headache We Fix (And How It Creeps In)
Lip wear is the most frequent problem we see, responsible for over 60% of the seal failures we troubleshoot at our tech support desk. It makes sense: the seal’s thin, flexible lip is designed to ride tight against a rotating or reciprocating shaft, creating a micro-thin barrier that keeps lubricant in and contaminants out. Over time, that lip degrades, either from material breakdown or friction that wears it away.
We recently worked with a farm equipment dealer who’d replaced 15 hydraulic pump seals on corn harvesters in a single harvest season—way above the typical 1,500-hour seal life they’d come to expect. When we pulled the failed seals, we found the problem was two-fold: the dealer had ordered standard nitrile rubber seals instead of the high-heat, high-abrasion silicone-bonded nitrile we recommend for dusty farm fields, and the shaft’s surface finish was too rough (12 Ra, instead of the required 2–6 Ra). The rough shaft acted like sandpaper, stripping the seal lip’s protective coating every time the harvester cranked up. We walked their maintenance team through testing shaft finish with a simple pocket gauge and adjusted their spec to match field conditions, and their seal replacements dropped to one a month after that.
Lip wear isn’t just about material choice, though. Even a perfectly matched seal will wear fast if the shaft misaligns. We had a mining client who kept replacing wheel hub seals on their dump trucks, only to learn the axle housing had a 0.008-inch runout that let the seal lip flap instead of sitting flat. That small amount of movement caused the lip to scrub unevenly, wearing through in weeks instead of months.
2. Contamination Ingress: The Silent Saboteur Most Teams Miss
If lip wear is the noisy, obvious failure, contamination ingress is the slow killer that creeps up on you. Contaminants—dirt, metal shavings, water, even tiny pieces of hydraulic fluid additive—work their way past the seal, and over weeks or months, they erode the shaft surface, scratch the seal lip, and mix with lubricant to create a gritty sludge that grinds everything down.
A prime example is the construction industry, where jobsites are perpetually dusty and muddy. We supplied seals to a concrete mixer fleet that was losing lubricant from their gearboxes at a rate that made quarterly oil changes insufficient. When we audited their sites, we found their gearbox breathers were missing—so as the mixer heated and cooled, air was drawn into the housing, carrying concrete dust right past the seal’s outer edge. The dust packed into the seal’s inner cavity, acting like an abrasive paste against the lip. Adding simple breathers and switching to a seal with a double-lip design (one primary lip for lubricant, one secondary scraper lip for external contamination) cut their lubricant loss by 85% in three months.
Even in clean, industrial settings, contamination can sneak in. A food processing plant we partner with uses stainless steel equipment, and they once had a batch of spoiled product linked to a gearbox seal failure. Turns out, they’d washed down the line with high-pressure hoses, and water had pushed past their standard single-lip seals during the cleaning process. We suggested FDA-compliant seals with a garter spring that’s coated in a water-repellent material, and added a vented cavity that let trapped water drain out before it damaged the lip. No more seal-related product spoilage after that.
3. Improper Installation: The Mistake That Ruins a Perfect Seal (Every Time)
I can’t count how many times we’ve unboxed a brand-new, high-quality seal only to see it fail a week later—all because it was installed wrong. Installation errors account for around 25% of seal failures, and most of them are avoidable with a little care.
The most common installation mistake is “hammering the seal in.” Techs often grab a pipe or a screwdriver and whack the seal into the housing, which can crack the seal’s metal case, fold over the thin lip, or leave burrs on the housing edge that tear the lip when it’s pressed in. We had a packaging equipment customer who tried to install 50 seals in one afternoon with a regular hammer; half of them failed within 10 hours of operation. We brought over our installation tool kits—simple, cheap blocks of wood or plastic that match the seal’s outer diameter, so you tap it evenly around the edge instead of hitting it in the middle—and showed their team the right way to seat seals. After that, their installation failure rate dropped from 40% to zero.
Another underrated installation error is ignoring the seal’s orientation. Seals have a specific side facing the lubricant, and if you flip it, the garter spring (the metal ring that holds the lip tight against the shaft) ends up on the wrong side, so it can’t create a proper seal. A textile plant once installed a batch of seals backward on their loom rollers, and by the end of the first shift, all of them were leaking lubricant onto their fabric rolls, ruining $20,000 worth of material. We now mark every seal package with a bold “LUBE SIDE IN” stencil, and we run a free online installation tutorial for all our customers to avoid that kind of loss.
4. Material Incompatibility: The Seemingly Perfect Seal That Destroys Itself
Material incompatibility is a tricky problem because the seal looks fine when it’s installed, but it starts breaking down chemically within days. It happens when the seal material reacts with the lubricant, fuel, or process fluid it’s meant to hold, causing the rubber to swell, crack, or harden until it can’t do its job.
We had a marine engine customer who used standard nitrile seals on their auxiliary engine’s fuel pump, only to find the seals were turning into soft, gummy goop after a month at sea. Nitrile is great for mineral oil-based lubricants, but it reacts with the biodiesel blend the customer had switched to for compliance with new environmental rules. We swapped them for fluoroelastomer (Viton) seals, which are resistant to biodiesel and most industrial chemicals, and their seal life extended to six months—well beyond the engine’s maintenance cycle.
Even temperature can cause material incompatibility. A plastic molding plant we work with had seals on their injection mold barrels that were cracking after just two weeks. The nitrile seals they’d ordered had a maximum temperature rating of 250°F, but the molding process ran at 280°F, so the rubber became brittle and cracked. We switched them to high-temperature silicone seals, rated for up to 350°F, and the problem was solved. The takeaway here is simple: always check the seal material specs against the full operating conditions, not just the fluid it’s holding.
What This Means For Your Operations
The biggest lesson I’ve learned as a seal supplier is that there’s no one-size-fits-all solution to oil seal problems. A seal that works perfectly on a farm harvester will fail on a construction dump truck, and a seal that’s cheap upfront will cost you thousands in downtime if it’s not matched to your needs.
Cogged V Belt At our company, we don’t just sell seals—we offer free site audits, material testing, and installation guidance to make sure our customers avoid these common mistakes. If you’re dealing with recurring seal failures, unexpected lubricant leaks, or downtime that’s cutting into your production, let’s talk. We can walk through your specific setup, test your current seals, and help you find a solution that works for your operations. No generic specs, no pushy sales pitches—just practical advice from a team that’s been in your shoes, fixing these exact problems for years.
References
- "Handbook of Fluid Sealing Technology," 5th Edition, Society of Tribologists and Lubrication Engineers, 2021
- "Failure Analysis of Elastomeric Seals in Industrial Applications," Journal of Tribology, Vol. 142, No. 8, 2020
- "Seal Installation Best Practices for Rotating Equipment," Maintenance Technology Magazine, 2022
- "Material Compatibility Guide for Rubber Seals," American Gear Manufacturers Association, 2019
Xingtai Boshuo Auto Technology Co., Ltd.
Xingtai Boshuo Auto Technology Co., Ltd. is one of the most professional oil seal manufacturers and suppliers in China, featured by quality products and low price. Please rest assured to wholesale bulk customized oil seal made in China here from our factory. Welcome to contact us for pricelist and free sample.
Address: No. 58 Quannan East Street, Xiangdu District, Xingtai City, Hebei Province
E-mail: sherry1@bs-belt.com
WebSite: https://www.bsbelts.com/
