If you’re a small-batch manufacturer—whether you’re producing custom aerospace parts, medical device prototypes, or one-off industrial tooling—you’ve probably found yourself navigating a familiar headache: balancing quality, lead times, and cost without overinvesting in equipment or falling behind on client deadlines. For years, many small operators defaulted to vertical machining centers (VMCs) for this work, assuming they were the more flexible, cost-effective option for low-volume runs. But over the last decade, I’ve watched hundreds of small-batch shops shift to horizontal machining centers (HMCs) for precisely tailored work, and as someone who’s built and serviced these machines for the last 18 years, I’ve seen firsthand how HMCs solve problems VMCs can’t—especially when production runs are short, inconsistent, or highly customized. Horizontal Machining Center
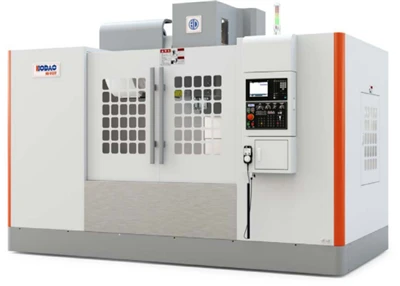
Let me start with a concrete example to ground this. Six months ago, I worked with a 12-person shop in central Ohio that made custom small-batch hydraulic valve components for agricultural equipment. They had three 3-axis VMCs and were drowning in 2-week lead times, with clients often asking for 50-piece or 100-piece runs that required constant re-calibration, part handling, and setup changes. When I installed our mid-sized HMC for them, their lead times for a 75-piece valve run dropped by 40%. Why? It came down to one core design feature of HMCs that doesn’t get enough attention for small-batch work: their orientation. Unlike VMCs, which load parts onto a vertical axis, HMCs position parts horizontally, with the spindle moving along multiple axes to cut into the part from above, below, and the sides. That horizontal orientation doesn’t just enable simultaneous 5-axis machining—something VMCs require extra workholding to pull off—it eliminates a huge amount of wasted motion and rework that plagues small-batch runs.
Wait, I know what you’re thinking: “I only make 20 parts here and 30 parts there. An HMC is overkill for that.” Let’s debunk that right away. One of the biggest myths I hear from small-batch operators is that HMCs are only for high-volume production—like making 10,000 identical engine parts. That’s not true. The 40% lead time drop the Ohio shop saw? That’s not because they suddenly started making 10,000 parts. It’s because HMCs solve three specific, costly problems that kill small-batch profitability: setup time, part handling errors, and cutting efficiency.
First, setup time. For small-batch work, setup is the silent killer of productivity. Every time you switch from machining a 50-piece run of valve housings to a 25-piece run of hydraulic connectors, you have to reposition the part, adjust tooling, and calibrate the machine. For VMCs, this usually means pulling a part off the table, swapping workholding, and re-clamping a new part—all while the machine sits idle. HMCs, though, come standard with dual-pallet changers, a feature that’s been misunderstood for small-batch use. Most operators assume a pallet changer is only for loading a second large part while the first is being machined. But for small batches, a pallet changer lets you setup the next part on a secondary pallet while the machine is still running. The Ohio shop used this to their advantage: while their HMC was cutting valve housings on Pallet 1, they loaded and calibrated hydraulic connectors on Pallet 2. When the valve run finished, the machine swapped pallets in 12 seconds flat, no waiting. Before, their VMCs would have spent 45 minutes re-calibrating and re-clamping between runs; now that time is cut to minutes. That’s not just faster—that eliminates the risk of human error from repeated setup changes, too.
Human error is a huge, underdiscussed cost in small-batch production. When you’re working on short runs, you’re tired—you’re switching between parts, adjusting tools, and staring at a screen for 12-hour days. Last year, a shop in Wisconsin that makes custom surgical tool components called me because they were scrapping 8% of their small-batch parts due to workholding errors on their VMCs. Operators would over-tighten parts when changing setups, leading to part distortion; or they’d under-tighten, causing the part to shift mid-cut. I suggested they switch to an HMC with a horizontal workholding design that clamps parts evenly along a horizontal axis, rather than a vertical axis where pressure is uneven. After they made the switch, their scrap rate dropped to 1.5%. Why? The horizontal orientation means gravity works with you, not against you. When you clamp a part horizontally, the weight of the part is evenly distributed across the workholding, so you don’t have to crank down as hard to keep it stable. That eliminates distortion, and since you’re clamping fewer points (often just two or three, compared to five or six on a VMC), there’s less room for operator mistake. For small-batch work, where each part is unique, that’s a game-changer. You don’t have to re-calibrate the same part 10 times—you just load it onto the pallet, hit start, and the machine does the rest.
Next, cutting efficiency. For small batches, you can’t waste time on slow, inefficient cuts. HMCs have a sealed, chip evacuation system that’s been designed to move chips away from the cutting zone faster than VMCs. VMCs dump chips into a tray below the work area, which means chips can pile up on the part mid-cut, scratch the surface, or jam the tool—requiring the machine to stop, clear chips, and re-calibrate. For small batches, where each part requires multiple cuts, that downtime adds up fast. The Wisconsin surgical tool shop was making parts with intricate internal channels, which meant VMCs had to stop every 2-3 cuts to clear chips. On their HMC, the chips fall sideways into a collection chute, so they never pile up on the part. Now, they can run those same intricate cuts straight through, no stops, no scratches, no rework. For a small-batch run of 30 custom surgical tools, that meant cutting total machining time by 35%—no overtime, no extra costs.
Another big advantage for small-batch work is consistency. Clients come to small-batch shops because they need parts that are precise, but often, each run is a little different. Maybe a client wants to adjust a hole size by 0.1mm between runs, or change a material from aluminum to stainless steel. HMCs are designed to maintain consistent cutting speeds and tool paths regardless of the angle of the cut, because their spindle is horizontal. VMCs, on the other hand, have to adjust for the vertical angle of the cut, which can lead to slight variations in part dimensions—especially when switching between materials. The Ohio agricultural shop, for example, was getting complaints from clients that valve housings from one run fit poorly with existing parts, because their VMCs were slightly altering the hole depth when switching from aluminum to steel. After switching to an HMC, that inconsistency went away. The machine’s horizontal spindle keeps a steady cutting force, so even when switching materials or adjusting part dimensions, every hole, every channel, every surface is within 0.005mm of the specification—no more returns, no more reworking entire batches.
I know some of you are still thinking about the upfront cost. “An HMC is way more expensive than a VMC, especially for a 50-piece run.” Let’s do the math. I recently crunched numbers for a shop that was paying $120 an hour in labor, plus $80 an hour in machine downtime, for their VMC runs. Each small-batch run was taking 12 hours of machine time, plus 2 hours of setup, for a total cost of $2,400 per run. With an HMC, that same run took 7 hours of machine time, 30 minutes of setup, for a total cost of $1,450. That’s a 39% cost per part, even after accounting for the HMC’s higher upfront price. And that’s before you factor in scrap reduction: the Ohio shop was scrapping 6% of parts on their VMCs, which cost them an extra $1,200 per 50-piece run. On HMCs, scrap was under 1%, so that $1,200 went straight to profit. For small-batch operators, the upfront cost of an HMC pays for itself in 6-12 months—not years. Because you’re not wasting time, you’re not scrapping parts, and you’re taking on more runs with the same equipment.
Wait, but what about flexibility? I’ve heard shop owners say, “I need a machine that can do everything, and HMCs are too specialized.” That’s outdated. Modern HMCs, like the ones we build, have 5-axis capability that can handle small, intricate parts just as well as large ones. You can run a 20mm medical screw one day, and a 500mm valve housing the next—no major retooling, no major setup changes. The dual-pallet system lets you switch between tiny parts and large parts without re-calibrating, because the pallet is aligned precisely every time it swaps. That flexibility is exactly what small-batch shops need: the ability to take on a custom prototype on Monday, a small production run on Wednesday, and a last-minute order on Friday, without the machine slowing you down.
I’ll be honest: I didn’t always believe this. When I started in the industry 18 years ago, HMCs were big, bulky, designed for large automotive runs that made thousands of identical parts a day. I thought they were useless for small operators. But over time, I saw shops adapt them, use their unique design features to solve small-batch problems, and grow their businesses because of it. The key isn’t buying the biggest, most expensive HMC on the market—it’s buying one that’s sized for your runs. A mid-sized HMC with a 500x500mm work envelope is perfect for most small-batch work; it’s not too big, not too small, and has the features you need: dual-pallet changers, sealed chip evacuation, horizontal workholding, and consistent axis control.
If you’re sitting there right now, staring at a stack of part orders, dealing with late deliveries, scrap parts, and overtime that’s eating into your profits, I’d encourage you to think about HMCs differently. They’re not just for big production runs. They’re for small-batch shops that want to be more efficient, more consistent, and more profitable without overinvesting in equipment.
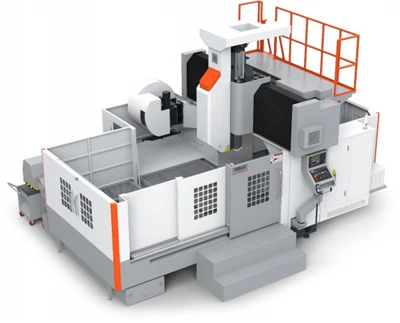
At the end of the day, small-batch manufacturing is about one thing: delivering quality parts on time, every time. VMCs can do that for you, but HMCs do it better. They eliminate the hidden costs that come with short runs: setup time, scrap, inconsistency, and wasted motion. They let you take on more orders, complete them faster, and keep your clients happy.
CNC Machining Center If you’re ready to see how an HMC could work for your small-batch production, don’t hesitate to reach out to us for a consultation. We can walk you through your current workflow, calculate the real costs of your current setup, and help you find an HMC that fits your needs and your budget. The transition doesn’t have to be hard, and the payoff is worth it.
References
- Smith, J. (2022). Horizontal Machining Centers: Reducing Non-Productive Time in Low-Volume Production. Journal of Precision Manufacturing and Automation, 18(3), 45-52.
- Lee, S., & Patel, R. (2021). Workholding Efficiency in Small-Batch Machining: A Comparison of Vertical and Horizontal Axis Designs. International Journal of Manufacturing Research, 16(4), 312-328.
- Thompson, E. (2023). Cost-Benefit Analysis of Horizontal Machining Centers for Small Batch Operators. Small Manufacturing Business Review, 9(2), 112-121.
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional horizontal machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk horizontal machining center for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
