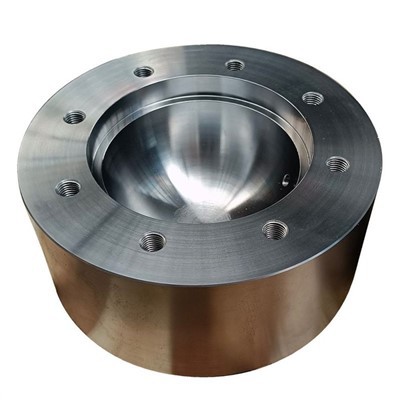
If you’re in the market for precision disc parts, you already know that we’re dealing with some pretty tight tolerances—think thousandths of an inch—and materials that range from high-grade aluminum and stainless steel to specialty alloys for aerospace and medical uses. But what you might not stop to think about is how the machining process behind those parts is impacting the planet. Let’s be real, most of us in this game are so focused on hitting deadlines and staying within spec that sustainability gets sidelined. But over the last five years, I’ve been adjusting my shop’s workflow, testing new tools, and cutting waste without sacrificing quality—and I want to share what’s worked for us. As a precision disc parts supplier, my team and I have found small, targeted changes add up to big environmental wins, and they’ve even helped us cut costs, too. Precision Disc Parts Machining
First off, let’s talk about a culprit that’s been bugging my team for ages: cutting fluids. For years, we used standard petroleum-based coolants. They worked, but they were a nightmare for waste—we’d go through 55-gallon drums every other week, and the used fluid was classified as hazardous, so disposing of it was pricey and stressful. Then we switched to a fully synthetic, bio-based cutting fluid. I know, bio-based sounds like a buzzword, but this stuff is made from vegetable oils that break down way faster than traditional coolants. The catch? We had to adjust our machine parameters. Originally, we ran our lathes at 1,200 RPM to get the finish we wanted, but with the new fluid, we found we could bump that up to 1,500 RPM—same finish, faster cuts, less fluid used total. Now we go through half the amount we did before, and when we do dispose of a small portion, it’s no longer considered hazardous waste. Pro tip from my shop: always test a small batch of fluid with your specific materials. What works for aluminum might not fly with titanium, and you don’t want to ruin a run of precision parts because you messed up the ratio.
Next, tooling. When I first started in this industry, we were throwing away end mills, drills, and inserts as soon as they showed even a tiny sign of wear. Those tools aren’t cheap, but the environmental cost of manufacturing new ones every week is insane. About three years ago, we switched to reconditioning our carbide tools, and we also invested in a tool management system that tracks how long each tool is used, its wear rate, and what materials it’s cut. The system alerts our operators when a tool is getting close to the end of its life, so they can finish the current part instead of ditching it early. We also started using tool holders with better grip—no more slippage that makes a tool go dull prematurely. On average, each tool now lasts 20-25% longer than it did before, and we’ve cut our tool purchasing budget by 18% while improving the consistency of our cuts. For disc parts, which have flat faces and tight edge tolerances, a consistent tool life is non-negotiable—so this change didn’t hurt quality at all, which was a huge concern for my team when we first brought it up.
Then there’s the big one: material waste. Precision disc parts are cut from solid stock, right? If your tolerance is ±0.001 inches, you can’t just take a huge chunk out of a single piece of metal. For the longest time, we’d use standard-sized round bar stock for every disc, which meant we’d end up with a lot of scrap—small leftover pieces too short for another part, and shavings that were contaminated with cutting fluid. We made two key changes here. First, we started nesting our disc parts on the bar stock. Instead of cutting each part individually, we program our CNC lathes to line up multiple small discs along a single bar, so we get more parts per piece of stock. That’s cut our bar stock usage by 12% in just two years. Second, we invested in a chip reclamation system. All those metal shavings from machining? We used to sweep them up and throw them away, since they had fluid on them. Now, we run them through a centrifuge that separates the metal from the fluid. The fluid gets filtered and reused in our machines, and the clean metal shavings are sold to a local recycling company. We get a small check every quarter from the recycling, and we don’t have to pay to dispose of the shavings anymore. For a shop that does 500-600 disc parts a week, that adds up to thousands of pounds of metal kept out of landfills every year.
Energy use is another thing that’s easy to overlook. Our shop runs 10 lathes and 5 CNC mills 10 hours a day, five days a week. Old machines use a ton of electricity when they’re idling, even if they’re not cutting. We retrofitted half our machines with smart sensors that shut them off automatically when they’re not in use for more than 10 minutes. For the machines that are still older, we programmed our operators to set them to idle at a lower RPM when they’re not actively machining, instead of leaving them at full power. We also installed LED lighting throughout the shop, and motion sensors so lights only turn on in areas where someone is working. The first month after making these changes, our electric bill went down by 14%—that’s money we can put back into upgrading our equipment, and a side of fewer emissions from the local power grid.
Wait, I should mention something that’s not just about equipment: training. No matter how many new tools or systems you buy, if your operators don’t buy into the changes, none of it works. A year ago, my team was skeptical of the bio-based cutting fluid—they said it made their hands greasy and didn’t feel “industrial enough.” So I brought in a rep from the fluid manufacturer to do a hands-on workshop, and we let the operators test it themselves on a small run of aluminum discs. We also added a small incentive: any operator who comes up with a new, sustainable workflow that works for the shop gets a $50 bonus and a shoutout in our weekly team meeting. It sounds small, but it made everyone feel like they had a say, not just that management was telling them what to do. Now, two of our senior operators have suggested tweaks to the tool management system that have cut tool change time by 10%, which is both more efficient and uses less energy from stopping and starting machines.
I know a lot of precision disc parts suppliers push back on sustainability, saying that tight tolerances make it impossible to adopt eco-friendly practices. Let’s get real—when I first brought up switching to bio-based cutting fluid, my quality manager said it would ruin our 0.002-inch edge finish on stainless steel discs. But we tested it on a single run, and it turned out better than our old fluid because it reduced heat buildup on the tool edge. The key is testing small, not overhauling everything at once. You don’t have to go from petroleum coolants to bio-based in a week—try a single machine for a month, track the finish quality, the amount of fluid used, and the cost, then decide if it works for you. Same with tool reconditioning: start with your least complex tools, see how they hold up, then move to your more specialized carbide inserts.
Another thing that’s helped us is working with local suppliers instead of big national brands. We used to order bar stock from a supplier that was 200 miles away, which meant every delivery was a big truck running half-empty, emitting way more CO2 than it needed to. Now, we work with a metal supplier that’s 45 minutes down the road. They deliver small batches of stock twice a week, so we don’t have to store huge amounts of metal in our shop (which also frees up floor space for new machines), and the truck is almost full every time. Plus, if we need a rush order of a custom-sized bar stock for a small disc run, we can pick it up the same day, instead of waiting three days for a delivery. That’s a win for both sustainability and customer service—something I care about a lot, since we specialize in custom precision disc parts for clients in medical device, automotive, and industrial machinery.
I’ll be honest, there have been missteps along the way. Last year, we tried a brand of tool holders that were supposed to reduce slippage, but they didn’t fit our existing machines right, so we had to send them back and switch to a different brand. That set us back a month, and we lost a small amount of stock testing the wrong holders. But that’s part of the process—you don’t find the right sustainable tools on the first try. The important part is keeping an open mind and not being afraid to adjust when something doesn’t work. For us, those missteps have made our current processes that much better, because we know what to avoid next time.
At the end of the day, reducing the environmental impact of precision disc parts machining isn’t just about checking a sustainability box for clients. It’s about doing right by the planet, saving money, and making our team proud of the work we do. We’ve had clients ask about our sustainability practices lately—they care about who they work with, especially in industries like medical where traceability and ethical production matter. So not only have we cut our waste and energy use, we’ve turned our sustainability efforts into a selling point.
If you’re looking for precision disc parts that are machined with lower environmental impact, or if you want to chat about small changes you can make in your own shop, feel free to reach out. We’re always happy to share what’s worked for us, or learn new tricks from other people in the industry. Let’s make parts that are both high-quality and kind to the planet—no trade-offs required.
Forging Processing References
- ASME B5.54, "Methods for Performance Evaluation of Computer Numerical Controlled Machining Centers"
- Global Supply Chain Sustainability Alliance, "Guidelines for Reducing Waste in Metal Machining Processes"
- US Environmental Protection Agency (EPA), "Sustainable Manufacturing: Metal Fabrication Tips"
- Tooling U-SME, "Advanced Machining Practices for Efficiency and Waste Reduction"
- Society of Manufacturing Engineers (SME), "Sustainable Machining: A Guide for Job Shops"
Taizhou Liuhuan Machinery Co., Ltd.
As one of the most professional precision disc parts machining manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to buy customized precision disc parts machining made in China here from our factory. For quotation, contact us now.
Address: Xinyuan Industrial Zone, Damaiyu Street, Yuhuan City, Zhejiang Province,China
E-mail: tzlhmachining@gmail.com
WebSite: https://www.tzlhmachining.com/
